Start With the Label Job and the End Use
Before you load a finishing module, match the setup to the label itself. A wine label, a snack label and a chemical label do not need the same release, adhesive trim or rewind handling, so the finishing plan should start with the stock, the web path and the final pack format.
Check whether the job is going out on rolls, sheets or finished packs, and confirm if the labels need slit lanes, matrix removal, serial marks or inspection after print. In Gauteng and the coastal provinces alike, humidity can affect web behaviour so allow for storage conditions and give the material time to settle in the pressroom if needed.
- Confirm label size, repeat and rewind direction.
- Check whether the job needs die cutting, slitting, sheeting or inspection.
- Confirm the required roll diameter and core size.
- Make sure the finishing path suits the adhesive and face stock.
Die Cutting, Slitting and Matrix Removal
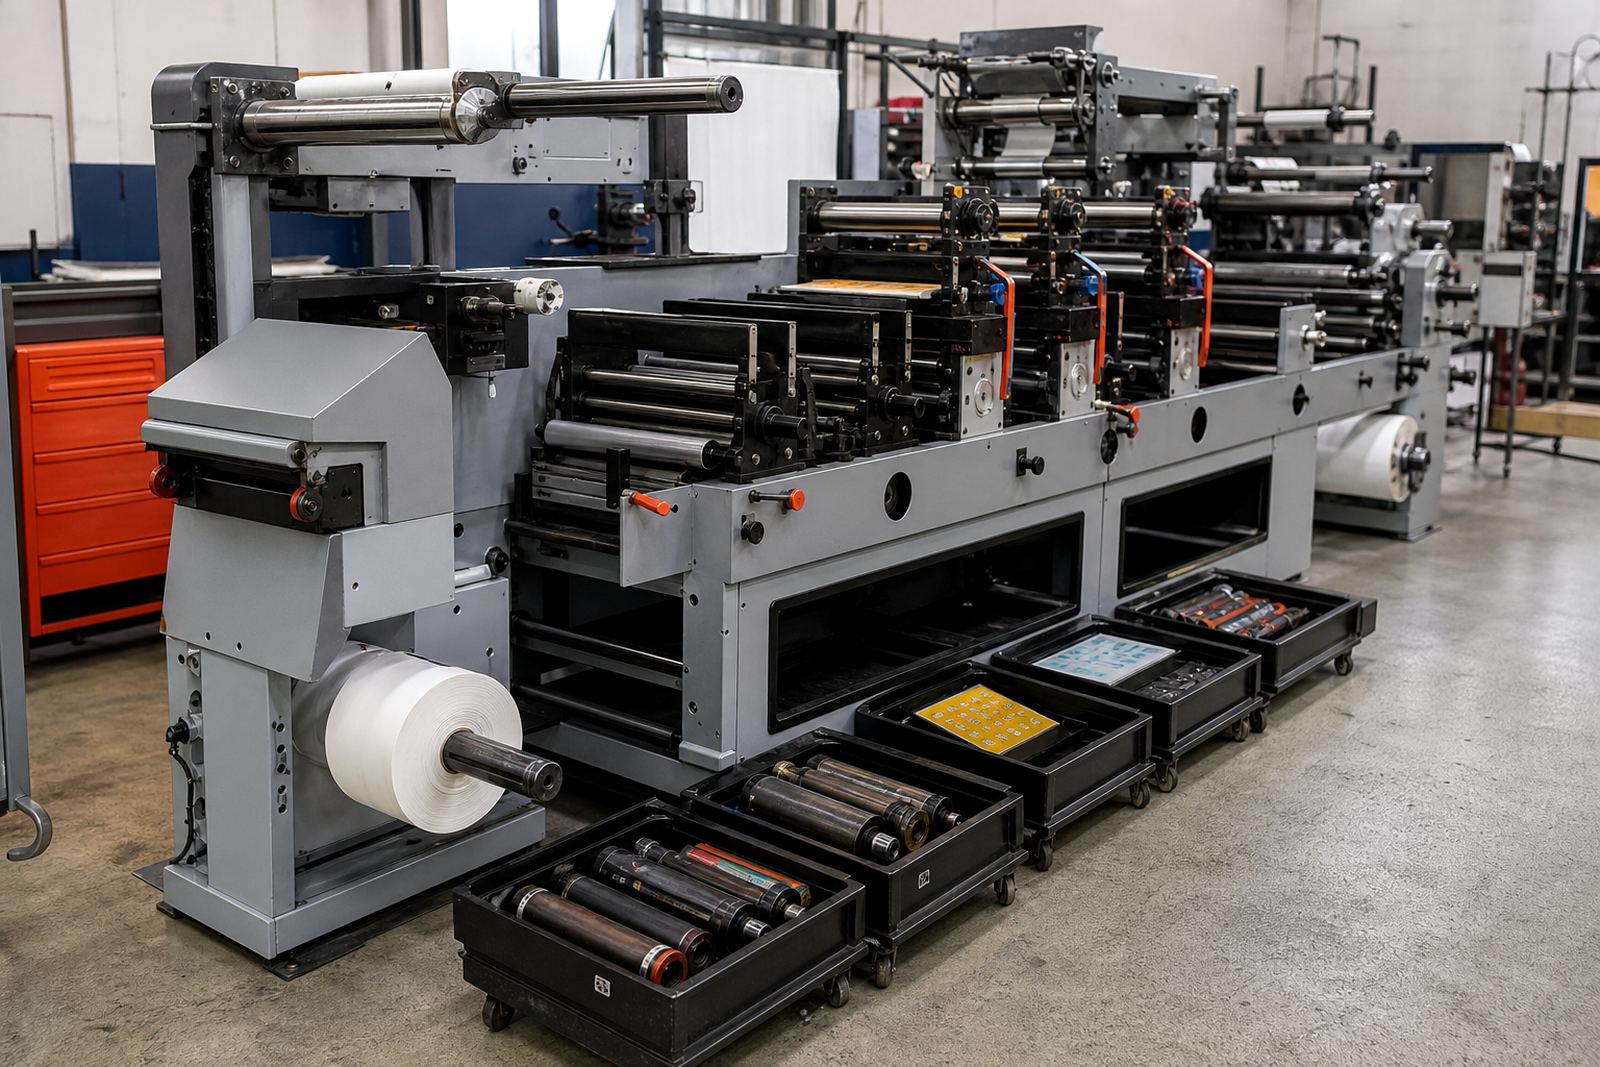
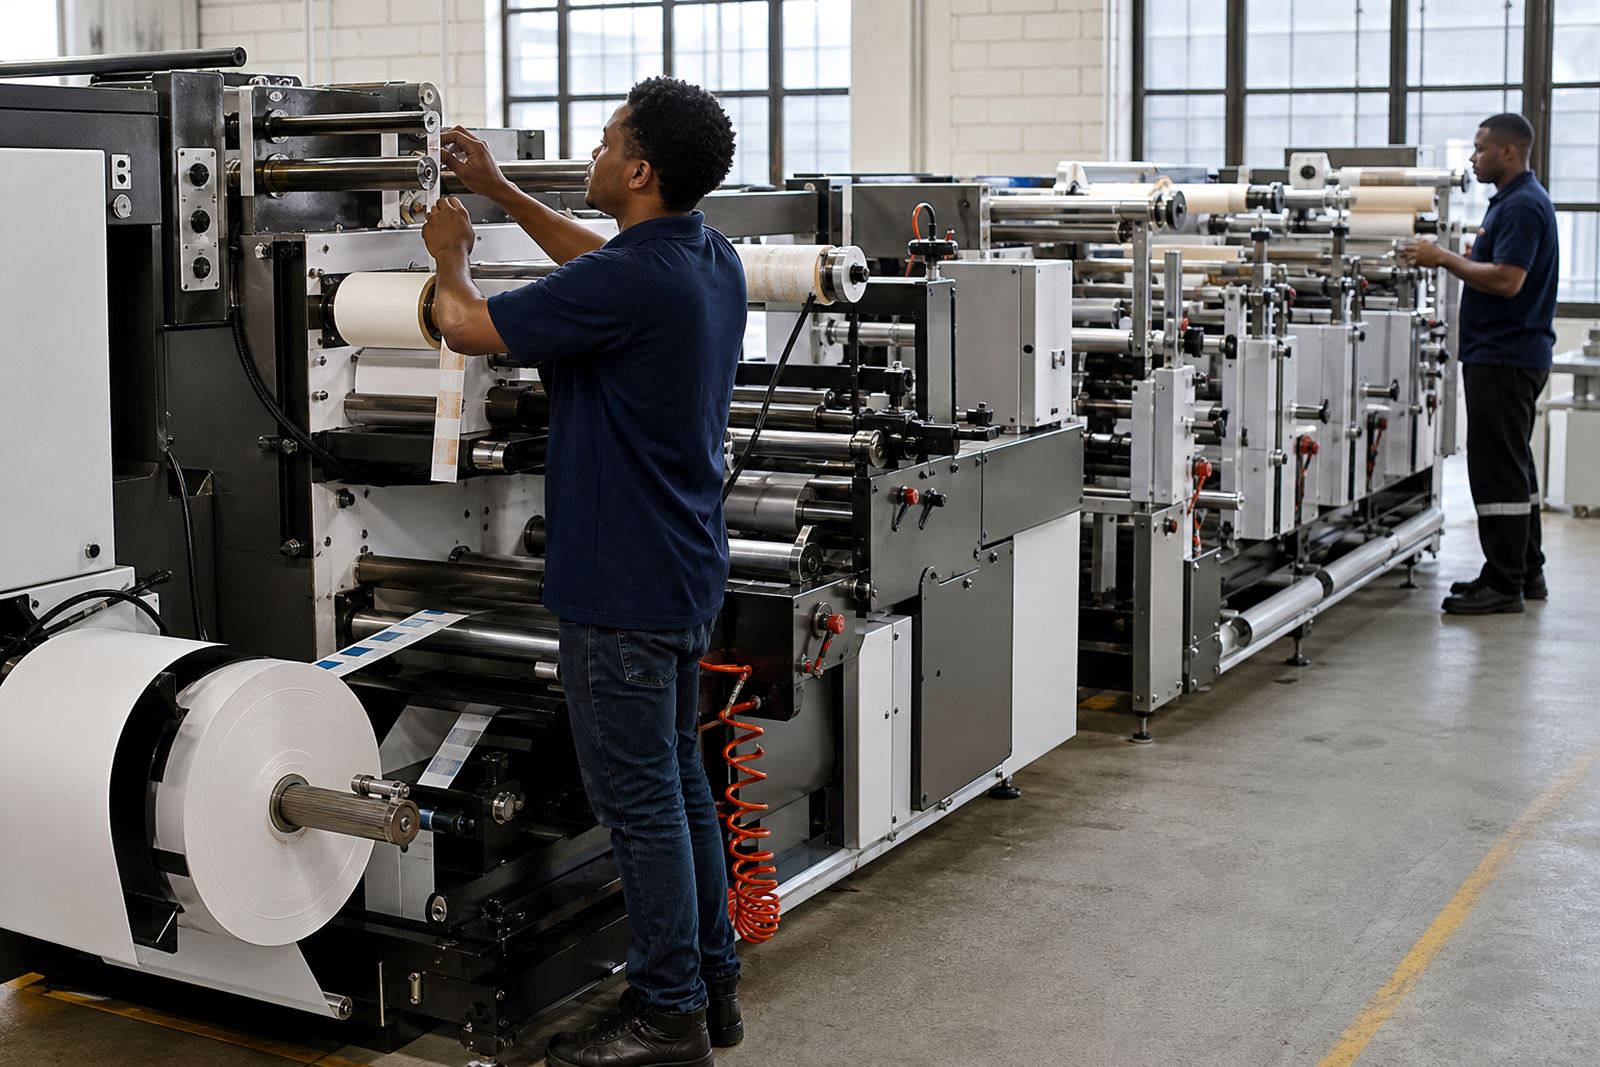
Die cutting is usually the first finishing step on a narrow-web line after print, with the cut made cleanly through the face stock without disturbing the liner more than needed. The important part is not speed alone, but keeping pressure even across the web so the cut stays consistent from edge to edge.
Slitting and matrix removal should be set up with care because a small fault here can cause wander, loose edges or waste buildup around the rewind. Keep blades sharp, check lane spacing and look for any signs of drag. If the waste does not clear properly, stop and reset before it turns into a longer problem.
- Check die pressure across the full web width.
- Inspect blade condition before each run.
- Keep waste paths clear and easy to access.
- Test a short length before committing to full production.
Lamination, Cold Foil and Surface Protection
Some finishing modules are there to improve appearance while others protect the label during handling and transit. Lamination can help with abrasion and moisture resistance, while cold foil or similar effects are used when the brief calls for added shelf appeal on cosmetics, beverages or premium retail packs.
Set the film or foil path carefully and watch tension at the unwind and rewind points. If the tension is too high, the web can stretch or the edges can pull out of line; too low and you may get wrinkles or uneven laydown. When working in coastal areas such as Durban or Gqeberha, keep an eye on static and moisture as both can affect adhesion and registration.
- Check web tension before the first production roll.
- Inspect the film or foil for wrinkles, lift or scuffing.
- Keep rollers clean and free of adhesive build-up.
- Run a short sample and check clarity, coverage and edge trim.
Inspection, Vision Checks and Rewind Control
Inspection modules help catch print faults before they leave the pressroom. They are useful for spotting missing print, colour shifts, splice marks and issues around variable data or repeated labels. Even on a well-set job, inspection gives the operator a second set of eyes and helps reduce waste at the finishing stage.
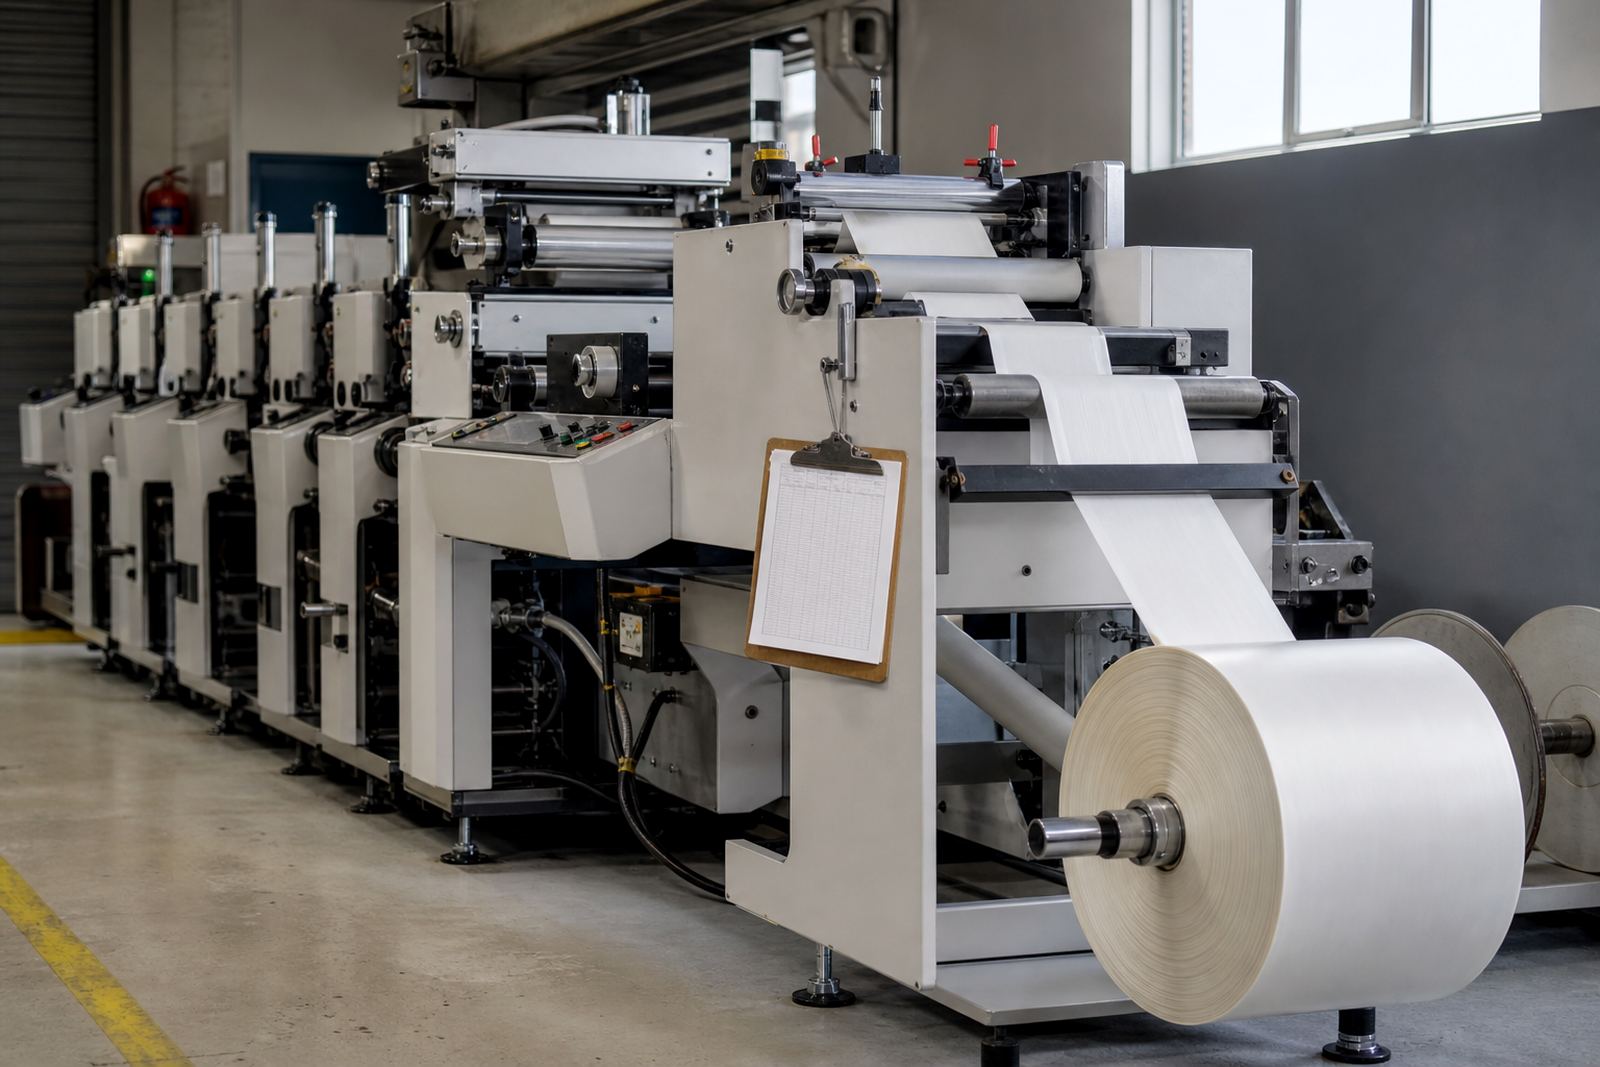
Rewind control matters just as much. A neat roll with even tension and firm edges is easier for the next process, whether that is packing, cartonising or dispatch. If the rewind is too tight, you can crush the roll or make unwinding difficult later. Too loose and the roll may telescope or slip in storage.
- Set the inspection camera or viewing point before production starts.
- Check the rewind core and roll build-up.
- Verify tension across the full width and not just the centre.
- Pull a sample roll and inspect the edge finish, core grip and flatness.
Setup Steps for a Clean First Run
A good first run begins with a clean web path and a simple check routine. This is where setup time pays off, because a small adjustment at the start can save a lot of scrap later. For label converters working under load-shedding pressure, it helps to finish these checks before the job is fully released so you are not resetting in the dark with a half wound roll.
Use the same order each time so the team develops a habit that works on the floor. The exact sequence may vary by module, but the aim is always the same: stable web control, correct cut, clean trim and a rewind that is ready for the next process.
- Thread the web and confirm the path through all active modules.
- Set tension from unwind to rewind, then test again at running speed.
- Check alignment at the die, slitter and rewind points.
- Run a short sample, inspect it, then approve full production.
Maintenance Checks That Keep Finishing Reliable
Finishing equipment needs routine care or it starts to show problems in the form of burrs, uneven cut quality, waste jams and poor roll build. A simple preventive routine is usually enough to keep most issues under control, especially where the same modules are used across different jobs in one shift.
Keep records of blade changes, roller cleaning, bearing checks and any adjustments made during setup. This makes it easier to spot patterns such as repeat faults on certain materials or roll sizes. It also helps when a technician needs to step in for breakdown support or remote support, because there is a clear history of what changed and when.
- Clean rollers and guides at the end of each shift.
- Inspect wear parts before they affect cut quality.
- Keep spare blades, cores and basic consumables close at hand.
- Log faults, adjustments and job-specific notes for the next run.
When to Call for Support on a Finishing Module
If a module keeps drifting out of registration, the waste will not clear properly or the rewind is coming off with soft edges, it is time to slow down and check the full setup. Some problems are simple operator adjustments, while others point to a mechanical issue that needs proper attention. Do not keep pushing through a fault hoping it will settle, because finishing problems can move quickly from nuisance to scrap.
We support label converters from Kempton Park, Johannesburg, Pretoria, Durban, Cape Town and Gqeberha with installation, commissioning, operator training, startup production support and spare parts support. If you need help with an inline finishing module, send your request through the enquiry form and we can work through the issue with your team.